A slitting line cuts a wide coil into narrower strips, and the equipment feeding it has to deliver consistent tension across the full width of the parent coil so every resulting strip comes off at the same quality.
Why tension control matters more on a slitting line
Any variation in feed tension shows up multiplied across a slitting line, because the single incoming strip is being divided into several narrower ones simultaneously. Uneven tension can produce strips with different camber or edge quality even though they came from the same parent coil, which is a problem a straight-through processing line doesn't have to the same degree.
Uncoiler/recoiler systems for feed and rewind
Pragya's uncoiler/recoiler systems handle coil weights from 5 to 60 ton, coil widths from 152–1829 mm, and material thickness from 0.4–3.4 mm, with coil OD up to 1400 mm. On a slitting line, the uncoiler feeds the parent coil into the slitter head under controlled tension, while recoilers on the exit side rewind the individual slit strips onto separate mandrels. Hydraulic mandrel expansion and variable-speed synchronized drives are what keep the tension consistent through the run, and coil slitting lines specifically are listed among the applications for this equipment. Where flatness defects or coil set survive the unwind, a plate leveler ahead of the slitter head corrects them — how leveling works.
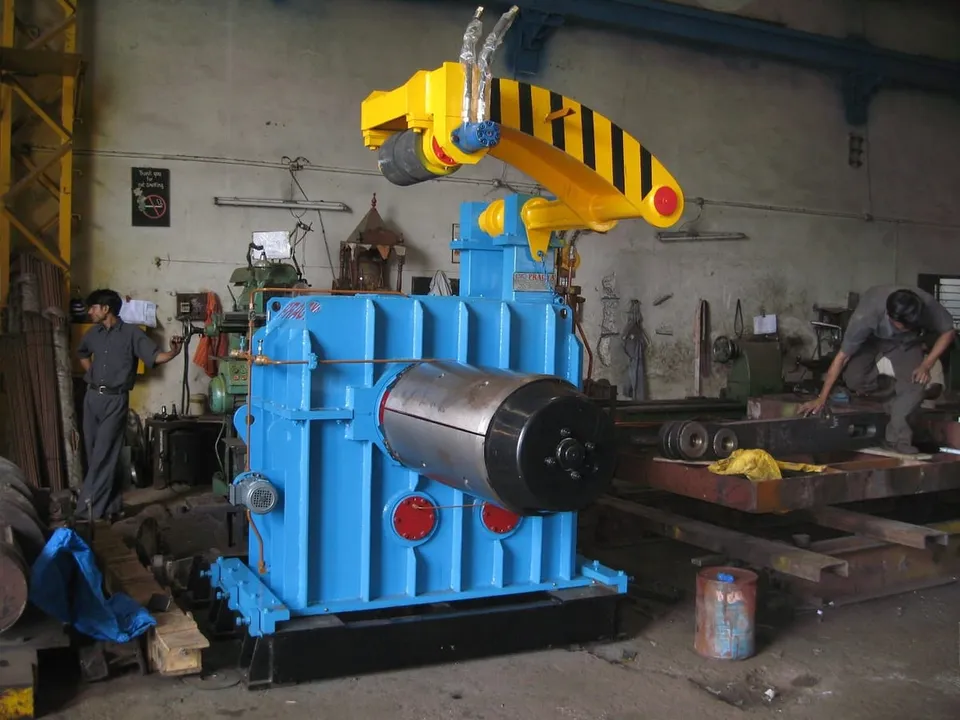
Turnstiles for coil accumulation and changeover
Slitting lines benefit from equipment that lets the next parent coil be positioned and ready before the current one is used up, minimizing downtime between coils. Pragya's turnstiles, rated up to 70 ton with 360° continuous rotation in manual or hydraulic actuation, serve this positioning role — bringing the next coil into alignment with the line so changeover happens quickly. This accumulation-and-positioning function is what keeps a slitting line's overall throughput closer to its theoretical line speed rather than losing time to changeover on every coil — more on the turnstile's role in coil and strip processing lines. Ahead of the line, a coil tilter presents the coil eye-out for uncoiling.
Matching equipment to strip width range
Slitting lines often run a wide range of final strip widths from the same set of equipment, so uncoiler/recoiler width capacity and turnstile capacity both need headroom for the widest parent coil the line will ever process — not just the most common one. Getting this wrong on the recoiler side in particular is a common oversight: an uncoiler sized correctly for the parent coil but paired with recoiler mandrels that can't handle the resulting strip range limits what the line can actually run.
Coordinating the two ends of the line
Because a slitting line's uncoiler and recoilers operate together — one parent coil in, several narrower strips out — the tension control on both ends needs to be coordinated rather than specified independently. A recoiler running slightly out of sync with the uncoiler's feed rate will introduce tension variation into the strip even if each piece of equipment performs correctly on its own. This is one of the reasons it's worth sourcing the uncoiler and recoiler as a matched system from a single supplier who can tune both to the same line speed and gauge range, rather than pairing equipment from different sources and hoping the control systems reconcile automatically. Bring your line speed and gauge range to our engineering team before splitting the order.
Export Availability
Manufactured at Pragya's Pithampur (Indore) works and exported to steel mills worldwide — 22+ countries across 5 continents to date. Every export order ships with mill test certificates, ocean-freight packing, and full customs documentation, quoted FOB or CIF.
Interested in our industrial equipment?
Our export team, based in Indore, India, will recommend the right solution and quote FOB or CIF pricing for your shipment.
Request a quote